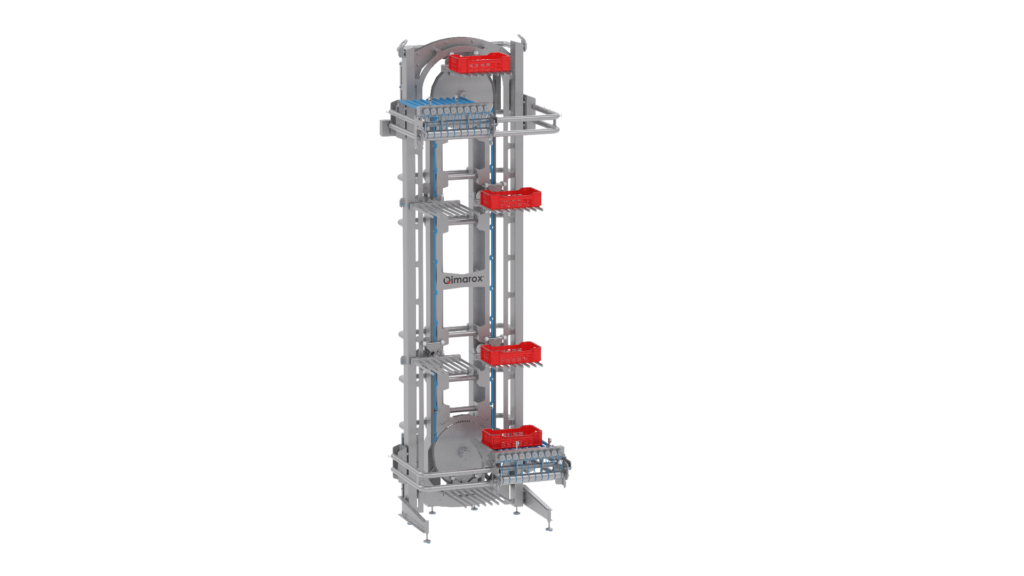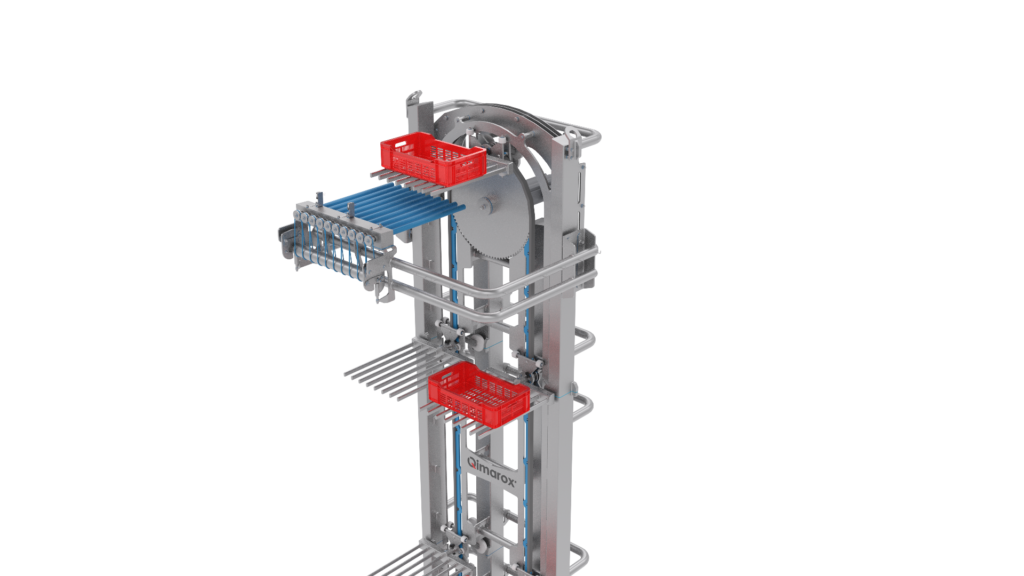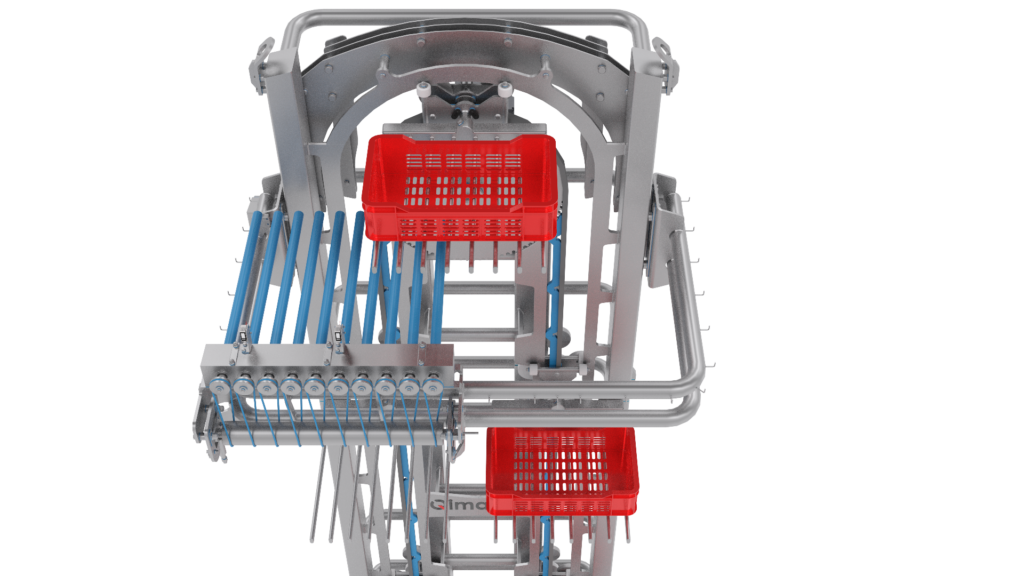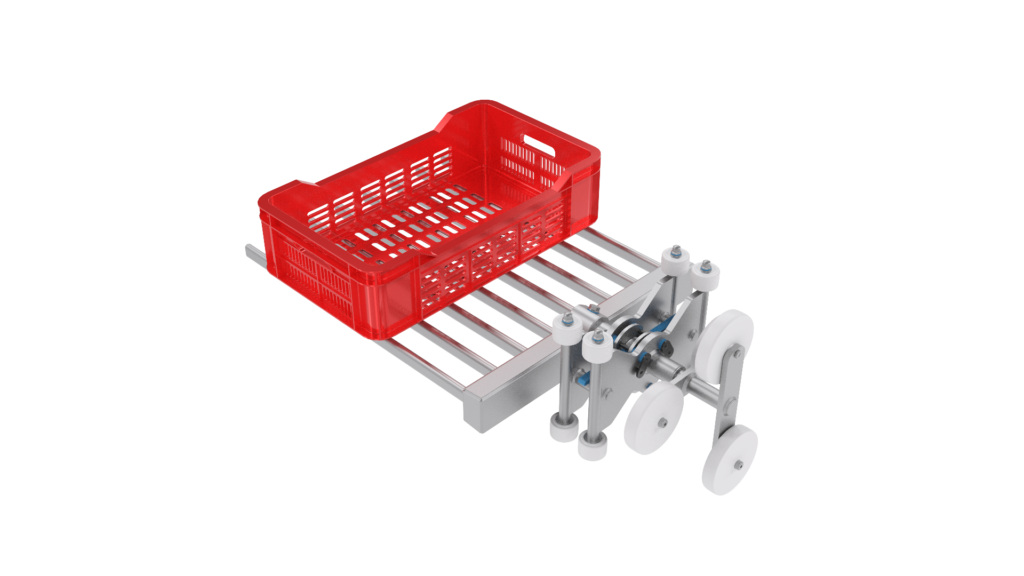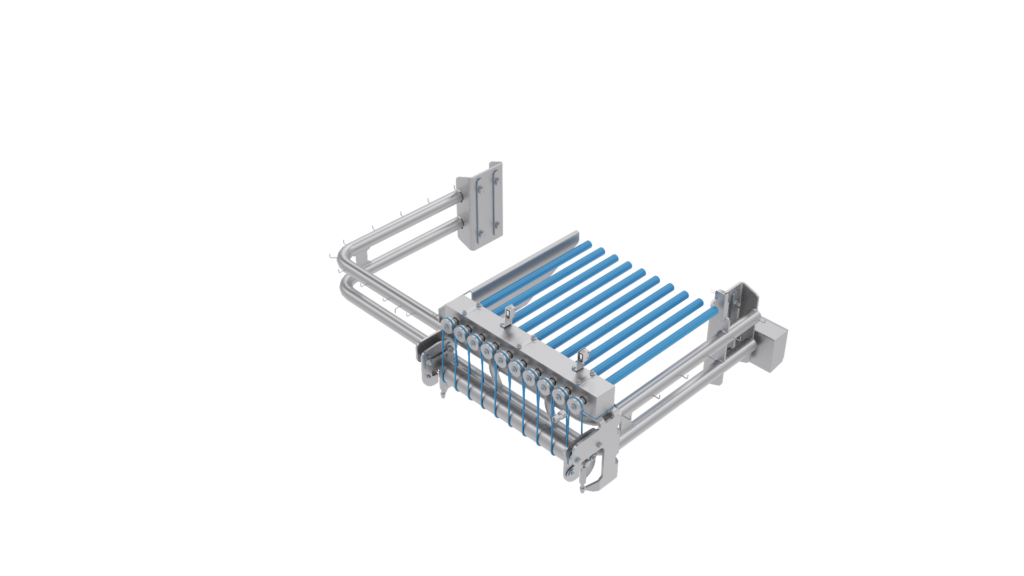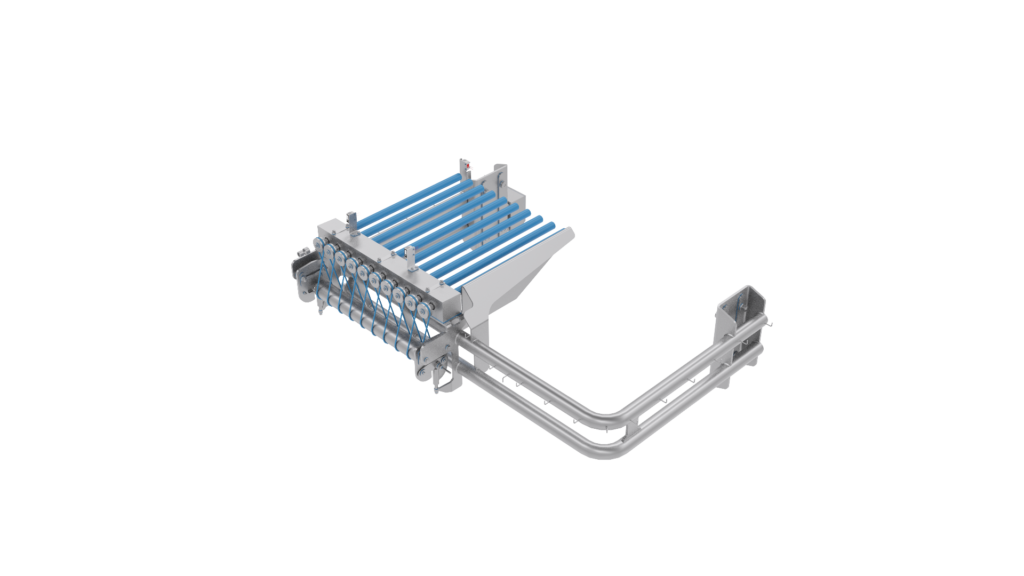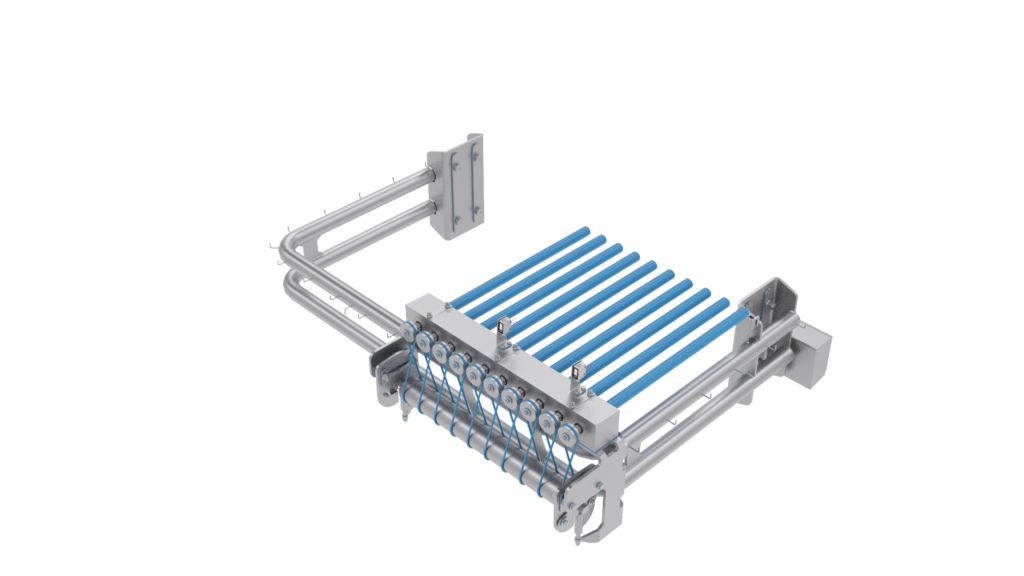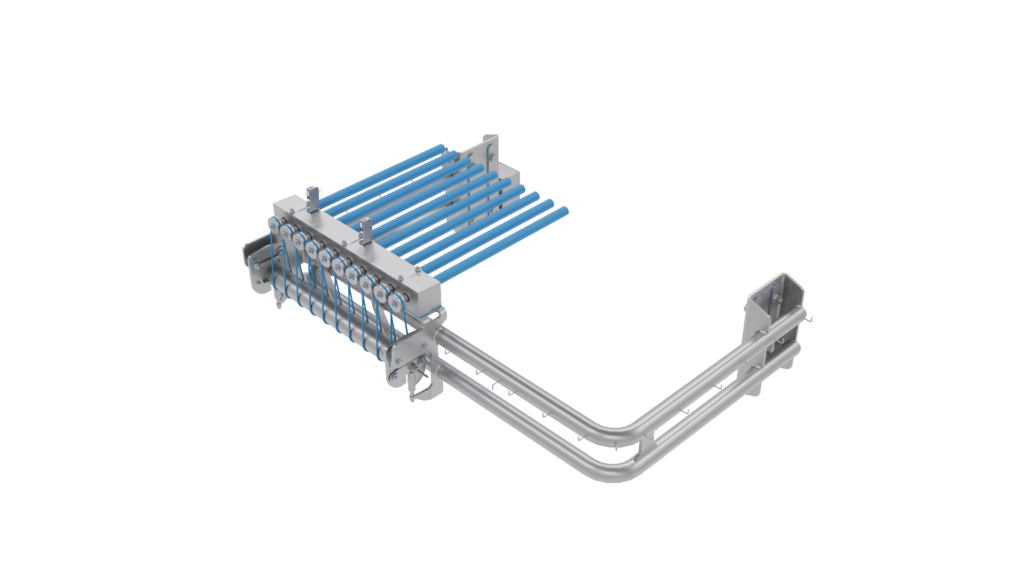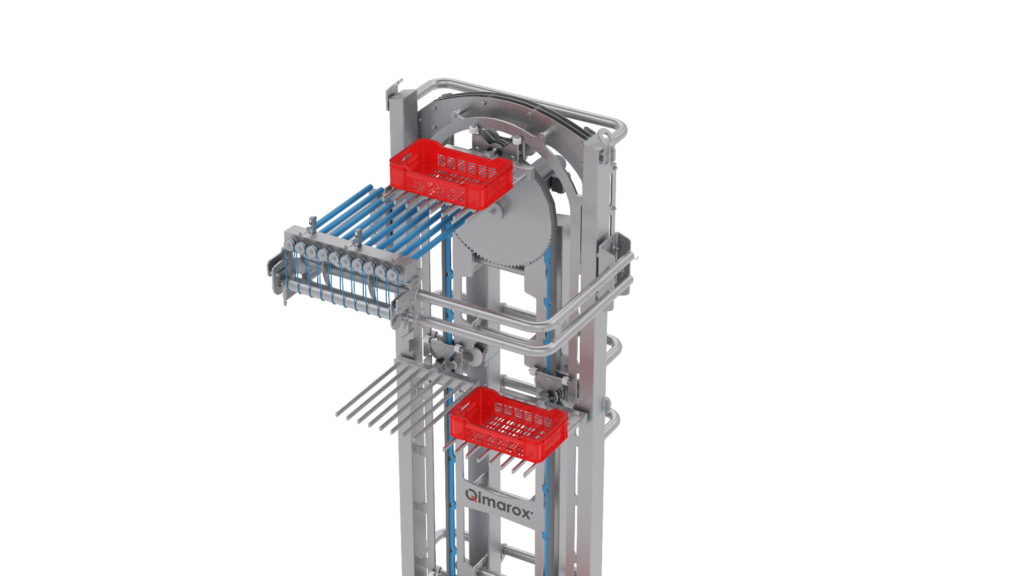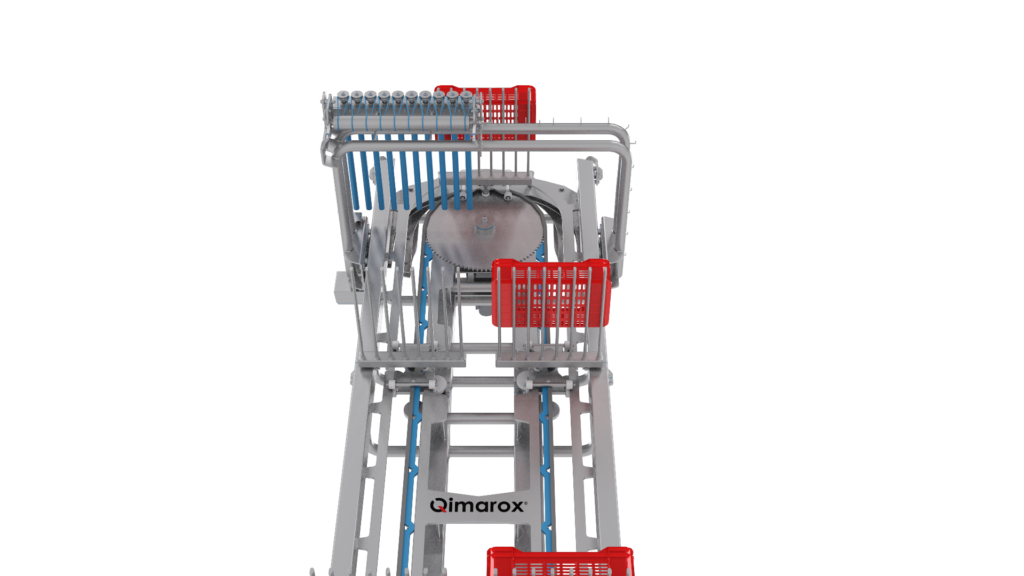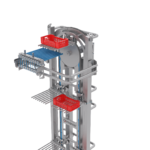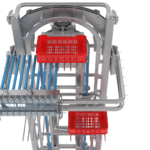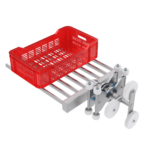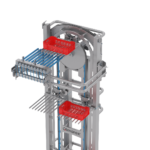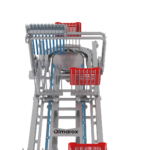

The Prorunner MK5 Hygiene is a hygienic continuous vertical conveyor for food, pharma, and clean environments. Easy to clean, modular, and reliable
The Prorunner mk5-Hygiene is a fully washable, continuous vertical conveyor designed for demanding hygienic environments such as the food and pharmaceutical industries. Built according to strict hygiene standards, this system enables efficient vertical transport without compromising cleanability, safety, or product integrity.
With its continuous operation and robust open design, the mk5-Hygiene combines high capacity with gentle product handling—making it ideal for modern automated production lines.
Why Choose the Prorunner mk5-Hygiene?
The PRmk5-Hygiene stands out as a robust, hygienic, and versatile vertical conveyor that meets the highest standards in cleanliness and efficiency. Its continuous motion ensures reliable throughput, while its hygienic design reduces downtime and simplifies cleaning procedures.
Whether you need to elevate packaged food, transfer products between levels, or integrate a vertical sorter into your line - the Prorunner mk5-Hygiene delivers consistent, high-performance results.
Why choose Qimarox?
Qimarox is a leading manufacturer of components for material handling systems. As a manufacturer of palletisers and product lifts, Qimarox distinguishes itself with a contemporary vision and approach. Innovation, quality and added value are of paramount importance. For more information about the Qimarox solutions take a look at our Vimeo channel.
Interested in this vertical conveyor - or a different conveyor solution?
If you would like more information about our vertical conveyor solutions, you can request a sales enquiry without any obligations. If you have any other questions please feel free to contact us!
Also explore other Prorunner models for your specific application.
The Prorunner mk5-Hygiene is suitable for a wide range of industries and products, including:
- Unpacked food
- Meat
- Frozen foods and packaged food products
- Cartons, trays, and totes
- Bags
- Shrink-wrapped goods
- Packaged bottles
- Soft parcels and boxes
Its hygienic design makes it particularly well-suited for environments where contamination control and frequent cleaning are essential.
- Capacity: up to 1100 products/hour
- Maximum product weight: approx. 110 lb
- Maximum throughput footprint: approx. 12 sq ft
- Maximum height: up to 49 ft
- Product sizes: flexible, with optional XL configurations available
Configuration Options
Flexible Layout
- Integrated reject option
- Available in C-lift and Z-lift configurations
- Multi-level infeed and discharge (vertical sorting)
- Can be configured for ascending or descending product flow
Integration Possibilities
- Compatible with driven or gravity conveyors
- Options for safety fencing and sensors (Securyfence)
- Can be used as standalone or integrated into complete material handling systems


Key Benefits
Continuous and Efficient Transport
- No start/stop movements, ensuring smooth product flow
- High throughput of up to 2000 products per hour
- Capacity determined by number of carriers rather than speed
Designed for Hygiene
- Fully washable and suitable for CIP (Cleaning in Place)
- Open design for easy cleaning and accessibility
- IP65 rating, with critical components rated IP69K
- NSF H1 food-grade lubricants
- Materials compliant with FDA and EU 10/2011 regulations
- Designed according to EHEDG guidelines
Flexible Integration
- Infeed and outfeed at multiple levels
- Supports line feed and cross feed
- Admits product from both the side and front
- Can function as a vertical sorter or cross transfer system
Reliable and Product-Friendly
- Carrier always remains horizontal
- No critical product transitions
- Suitable for delicate or unstable products
- Low noise operation
- Drive system safely integrated within the column